Top Industrial Valve Manufacturers in China: A Comprehensive Guide to China's Leading Valve Industry
China has become one of the world's largest manufacturing centers for industrial valves, supplying products to oil and gas companies, EPC contractors, petrochemical plants, power stations, marine engineering firms, mining operations, and water treatment facilities across more than 150 countries. Thanks to decades of industrial development, advanced manufacturing technologies, and internationally recognized quality standards, top industrial valve manufacturers in China now compete successfully with many established European, American, Japanese, and Korean brands.
Whether you are sourcing API valves for an oil refinery, high-pressure forged valves for power generation, stainless steel ball valves for chemical processing, or customized valve solutions for large infrastructure projects, China offers a broad selection of manufacturers capable of meeting international engineering specifications.
This guide explores the strengths of China's industrial valve industry, major valve categories, manufacturing capabilities, quality standards, applications, and key factors buyers should consider when selecting a reliable supplier.
Over the past three decades, China has invested heavily in industrial manufacturing, metallurgy, precision machining, automation, and engineering research. As a result, Chinese valve manufacturers have significantly improved their technical capabilities while maintaining competitive production costs.
Today, many leading manufacturers export industrial valves worldwide because they offer:
- Advanced CNC manufacturing equipment
- Modern forging and casting technologies
- Comprehensive product portfolios
- International certifications
- Flexible customization
- Large-scale production capacity
- Competitive pricing
- Efficient global logistics
- Strong OEM and private-label capabilities
- Experienced engineering support
Many Chinese factories now manufacture valves that fully comply with international standards required by energy, chemical, and industrial projects.
Chinese manufacturers produce virtually every type of industrial valve used in modern process industries.
Ball valves are among the most widely used valves because they provide reliable shut-off performance, low operating torque, and minimal pressure loss.
Common types include:
- Floating Ball Valves
- Trunnion Mounted Ball Valves
- Top Entry Ball Valves
- Side Entry Ball Valves
- Fully Welded Ball Valves
- Metal Seated Ball Valves
- Cryogenic Ball Valves
- Three-Way Ball Valves
These valves are extensively used in pipelines, oil and gas production, LNG terminals, and chemical processing.
Gate valves provide full-port flow with minimal pressure drop and are widely installed where complete isolation is required.
Popular products include:
- Cast Steel Gate Valves
- Forged Steel Gate Valves
- Pressure Seal Gate Valves
- Knife Gate Valves
- Cryogenic Gate Valves
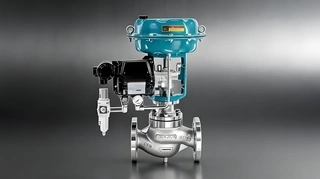
Globe valves are designed for flow regulation and throttling applications where accurate control is essential.
Typical applications include:
- Steam systems
- Boiler feedwater
- Chemical processing
- Power plants
- Industrial utilities
Check valves prevent reverse flow and protect pumps, compressors, and pipelines.
Common designs include:
- Swing Check Valves
- Lift Check Valves
- Dual Plate Check Valves
- Wafer Check Valves
- Tilting Disc Check Valves
- Axial Flow Check Valves
Butterfly valves are widely used because they are lightweight, economical, and suitable for large-diameter pipelines.
Applications include:
- Water treatment
- HVAC systems
- Fire protection
- Chemical plants
- Marine engineering
Plug valves provide reliable quarter-turn operation for handling corrosive, abrasive, and high-temperature media.
Forged steel valves are manufactured for severe service conditions involving high pressure and high temperature.
Typical products include:
- Forged Gate Valves
- Forged Globe Valves
- Forged Check Valves
- Forged Ball Valves
- Pressure Seal Valves
Material selection is critical to valve performance, service life, and safety.
Leading Chinese manufacturers commonly produce valves using:
- Carbon Steel
- Stainless Steel
- Duplex Stainless Steel
- Super Duplex Stainless Steel
- Alloy Steel
- Chrome-Moly Steel
- Bronze
- Brass
- Cast Iron
- Ductile Iron
- Monel
- Inconel
- Hastelloy
- Titanium
- Nickel Alloys
Special materials can also be supplied for highly corrosive, cryogenic, or high-temperature applications.
Modern industrial valve production combines advanced machinery with precision engineering.
Typical manufacturing capabilities include:
- CNC Machining Centers
- Vertical Machining Centers
- Five-Axis Machining
- Precision Turning
- Robotic Welding
- Heat Treatment
- Surface Finishing
- Automatic Assembly
- Digital Measurement Systems
- Coordinate Measuring Machines (CMM)
Many factories have adopted lean manufacturing and intelligent production systems to improve efficiency and product consistency.
Industrial valves supplied to global markets must comply with internationally recognized standards.
Common manufacturing standards include:
- API 6D
- API 600
- API 602
- API 608
- API 609
- API 594
- API 598
- ASME B16 Series
- ANSI Standards
- ASTM Material Standards
- ISO 9001
- ISO 14001
- ISO 45001
- MSS Standards
- EN Standards
- DIN Standards
- PED
- CE
- NACE MR0175
- ISO 15848 Fugitive Emission
Compliance ensures compatibility with engineering specifications used throughout the global energy and industrial sectors.
Reliable industrial valves depend on rigorous quality management.
Most leading manufacturers implement inspection procedures covering:
- Raw Material Verification
- PMI (Positive Material Identification)
- Chemical Analysis
- Mechanical Testing
- Forging Inspection
- Casting Inspection
- Dimensional Inspection
- Ultrasonic Testing (UT)
- Magnetic Particle Testing (MT)
- Liquid Penetrant Testing (PT)
- Radiographic Testing (RT)
- Hydrostatic Pressure Testing
- Seat Leakage Testing
- Air Leakage Testing
- Torque Testing
- Functional Testing
- Final Inspection
Many manufacturers also maintain complete material traceability throughout production.
Industrial valves produced in China support nearly every major industrial sector.
Key industries include:
Exploration, drilling, pipelines, refineries, storage terminals, and offshore platforms require valves capable of operating under extreme pressure and temperature conditions.
Petrochemical plants demand corrosion-resistant valves with excellent sealing performance and long service life.
Coal-fired, gas-fired, nuclear, biomass, and renewable energy facilities require high-performance valves for steam systems, condensate systems, and cooling water networks.
Liquefied natural gas processing requires specialized cryogenic valves designed for ultra-low-temperature service.
Chemical plants rely on valves manufactured from corrosion-resistant alloys capable of handling aggressive chemicals.
Marine valves must withstand seawater corrosion while maintaining reliable operation under harsh environmental conditions.
Mining operations require durable valves capable of handling abrasive slurries and demanding operating environments.
Municipal and industrial water treatment plants use butterfly valves, gate valves, check valves, and control valves for efficient flow management.
Selecting the right supplier involves more than comparing prices. Buyers should evaluate a manufacturer's technical capabilities, quality systems, and industry experience.
Key considerations include:
- Years of manufacturing experience
- Product range
- API certifications
- ISO quality management
- Engineering capability
- Manufacturing capacity
- Material availability
- Testing facilities
- Export experience
- Project references
- Lead times
- Technical documentation
- After-sales support
- Customization capability
A dependable manufacturer should also provide complete documentation, including material certificates, inspection reports, pressure test records, and compliance certificates.
China's valve industry continues to evolve in response to changing market demands and technological advancements.
Current trends include:
- Smart valves with digital monitoring
- Automated valve actuation systems
- Low-emission valve designs
- Hydrogen-compatible valves
- Carbon capture and storage applications
- Cryogenic valve technologies
- Advanced sealing materials
- Intelligent manufacturing
- Robotics and automation
- Digital quality traceability
- Sustainable production practices
These developments are helping Chinese manufacturers compete in increasingly sophisticated global markets.
Global demand for industrial valves is expected to continue growing as investments increase in energy infrastructure, LNG, hydrogen, water treatment, renewable energy, and industrial modernization.
Chinese manufacturers are responding by expanding research and development, upgrading production equipment, improving quality management systems, and adopting intelligent manufacturing technologies. These investments are enabling them to deliver higher-value products with improved reliability, tighter tolerances, and enhanced performance.
For international buyers, this means access to a broader range of industrial valve solutions backed by advanced manufacturing capabilities and competitive global supply chains.
China has established itself as one of the world's leading sources of industrial valves, offering a comprehensive selection of products for virtually every process industry. From ball valves and gate valves to forged steel valves, butterfly valves, globe valves, check valves, and specialized severe-service solutions, Chinese manufacturers combine modern production technology, international quality standards, and strong engineering expertise to meet the needs of global customers.
When selecting from the top industrial valve manufacturers in China, buyers should look beyond pricing and carefully evaluate manufacturing capability, certifications, quality assurance, material expertise, testing procedures, export experience, and technical support. By partnering with a qualified manufacturer, companies can secure reliable, high-performance valve solutions that contribute to safer operations, improved efficiency, and long-term project success.